Supply chain planning and operations for pharmaceutical manufacturing
Batch production, long lead times on materials, shelf life and no room for stockouts. We connect demand, production and material planning, set inventory by the risk it covers and design warehouses and processes around strict quality rules.
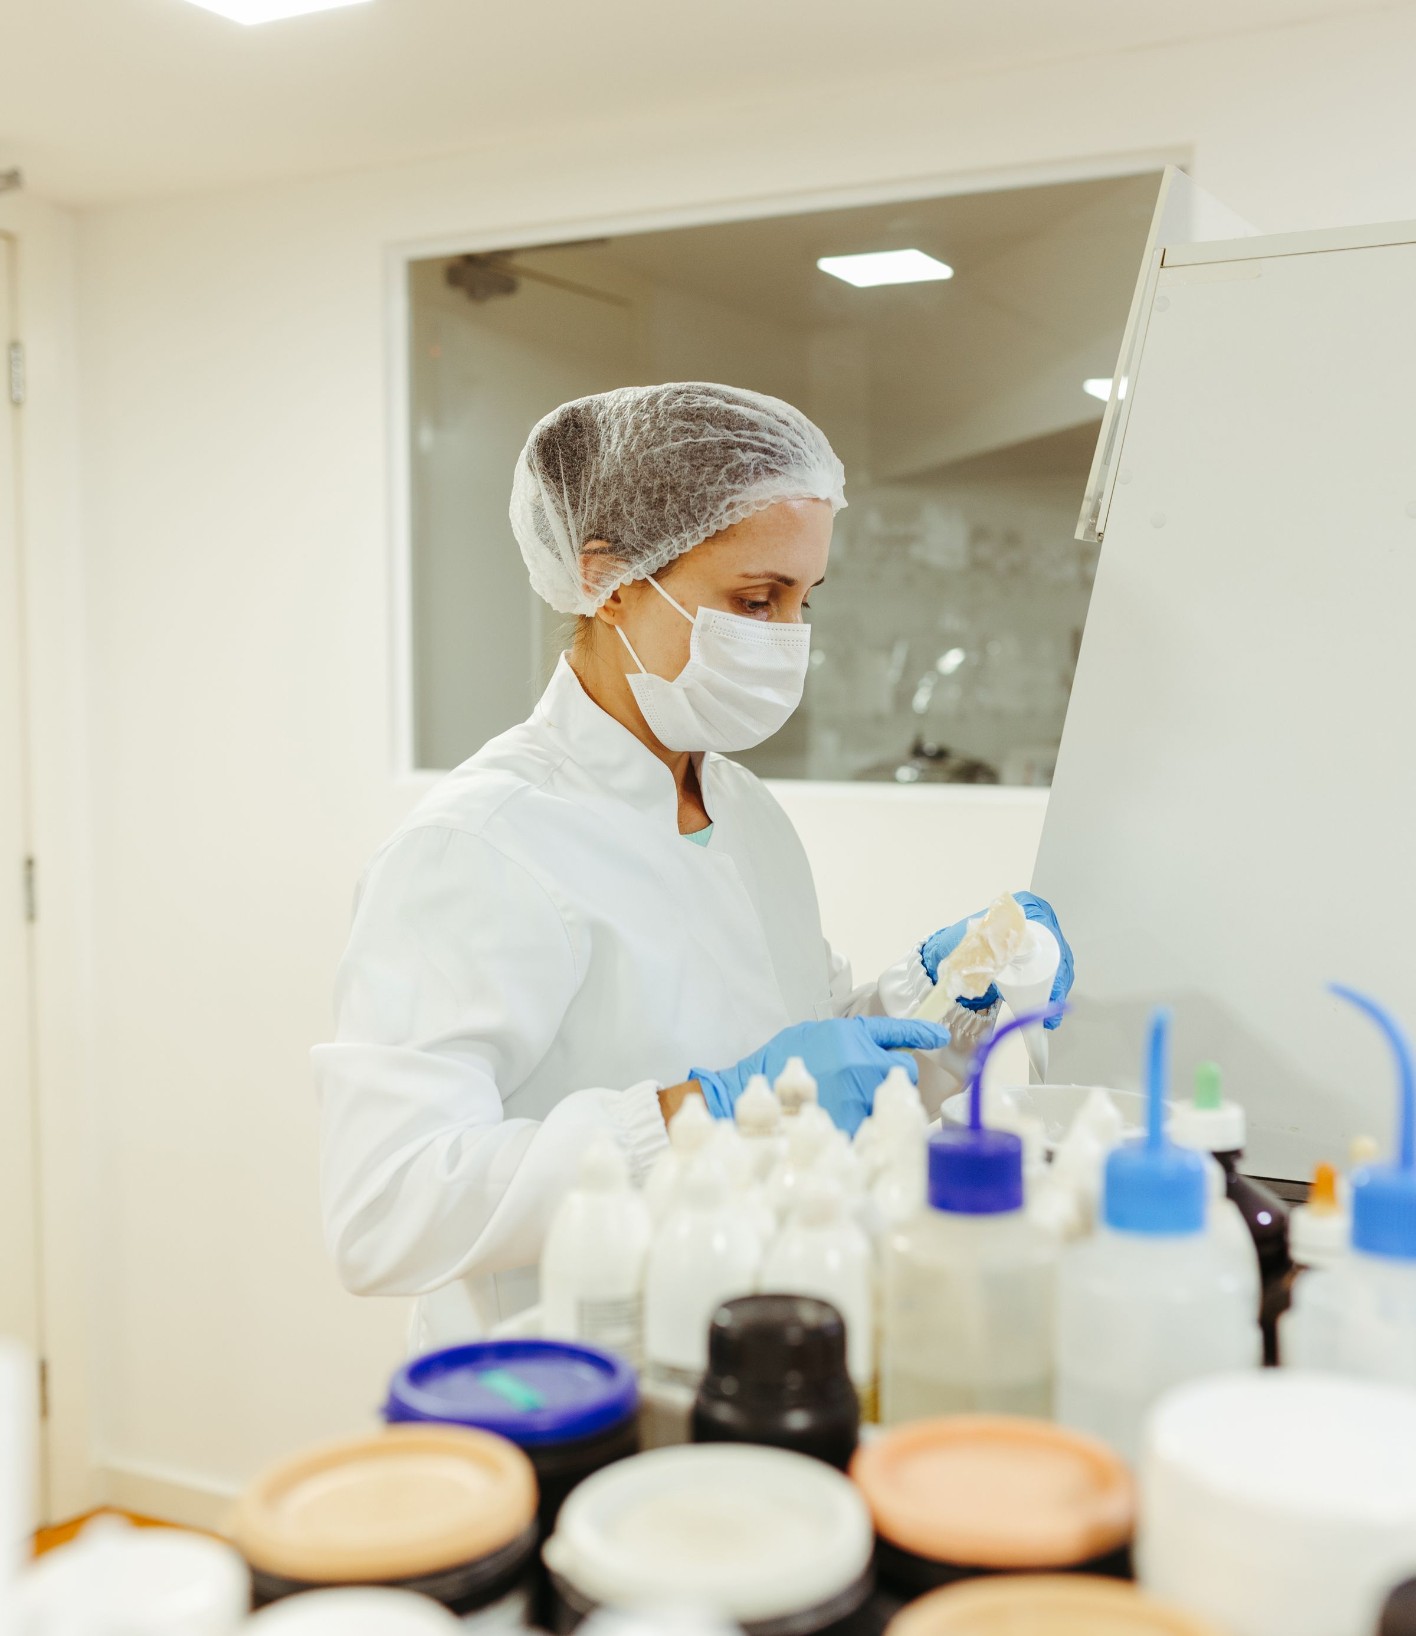
Outage risk from input‑material quality at Oncomed
−0%
Average stock at Oncomed, in pieces
−0
Inventory capacity at Oncomed
+0%
What pharmaceutical manufacturers deal with
Long material lead times
Active ingredients and packaging materials are ordered months ahead, while demand changes by market and tender.
Batches and changeovers
Campaign production and cleaning between batches make every change to the schedule expensive.
Shelf life
Materials and finished goods expire. Stock that waits too long is written off.
Buffers without a risk logic
Safety stock grows at every step because nobody knows which risk it covers.
What we solve as consultants
S&OP and planning processes
One plan from market demand to production and material purchasing, with clear roles and a regular rhythm.
Production capacity planning
Line capacity, batch sizes and changeovers aligned with the demand plan.
Inventory risk and purchasing
For Oncomed we mapped the flow from supplier to finished product and set purchasing controls that halved the outage risk.
Warehouses and material flow
Layout, storage rules and material flow for materials, work in progress and finished goods.
Maintenance and spare parts
Preventive maintenance and spare parts planned around the equipment that must not stop.
Veritico for pharmaceutical manufacturers
Demand forecasting
Forecast per item, market and warehouse, used for production and material planning.
Warehouse replenishment
Warehouse and distribution orders from the forecast, lead times and target service level.
Expiry‑aware ordering
Shelf life enters the order calculation, so stock is planned to be sold before it expires.
Service levels and safety stock
Target availability per product segment, with safety stock calculated to reach it.
Case studies
Inventory risk reduction for Oncomed
Value stream mapping and tighter purchasing controls helped Oncomed halve outage risk and release capacity with 60,000 fewer pieces held in stock.
–60,000 pcs average stock
–50% outage risk from input‑material quality
+14% inventory capacity
Faster spare‑parts search and clear stock visibility for Hartmann
Searchable spare‑parts database with clear stock visibility and daily Power BI reporting, saving admin time and simplifying decisions.
Up to 1 hour saved per day for the administrator
Questions about pharma manufacturing
Yes, when buffers are set by the actual risk. Oncomed halved the outage risk and reduced average stock by 60,000 pieces at the same time.
Yes. Shelf life enters the order calculation, and target service levels can be set per product segment.
With mapping the flow from demand to materials. It shows where stock and risk arise and whether the fix is a process, a plan or a system.
Talk to a pharma manufacturing expert
Tell us about your products, plants and where planning breaks down. We will suggest where to start.